
A lab dip is a laboratory-scale dye trial run before bulk production, to confirm the shade, control quality, and reduce the risk of off-specification colour in a large production lot.
When ordering fabric for industrial work, large dyeing and printing lots, or export production, "off-shade" and "out of specification" colour can lead to re-dyeing, late delivery, rejected goods and significantly higher cost. That is why a lab dip is a step both mill and buyer should complete before approving bulk production, every time.
What is a lab dip?
A lab dip is a laboratory trial in which a dye recipe is mixed and applied to fabric, before the approved recipe goes into industrial-scale bulk production.
The purpose is to model the outcome: what the customer’s reference colour will actually look like once it is dyed onto the specified fabric and construction. The mill then presents the lab dip sample for the customer to review, and the shade is agreed between both parties before bulk production starts.
Approving a lab dip is therefore not simply a check that the fabric looks close to the sample. It is the point at which a colour standard is set that everyone works to for the rest of the production run.


Why lab dips matter in the textile industry
Whether you are a major fabric trader, a cut-and-sew factory, a purchasing team or a brand owner, lab dip approval is the first line of quality-risk control. A small colour deviation carries downstream into cutting and sewing, product assembly, goods inspection and the supply chain as a whole.
A lab dip brings the customer benefit at several points — confirming the intended shade, reducing the risk of a production error, and controlling product quality against standard before bulk production begins.
Fewer misunderstandings, and less hidden cost
Confirming the shade from a real sample before production means mill and customer share the same understanding. That reduces the chance of an off-shade result requiring a re-dye, which costs time, raw material, energy and production capacity for no return.
Consistent colour across lots
An approved lab dip serves as the colour reference during production, reducing shade variation between dye vessels or between lots — known as shading. This matters most for fabric that will be cut and sewn into a single product, where a difference in shade can put the finished item outside the brand’s standard.
A reference standard for goods inspection
A customer-approved lab dip becomes a quality reference — a QC standard — for checking colour during production and at delivery. It gives quality decisions clear evidence to point to, for domestic and export work alike.
From visual assessment to digital colour measurement
Assessing colour by eye in a light box is useful, but visual judgement alone is affected by the surrounding environment, the light used, and differences in how individuals perceive colour.
Textile mills that need industrial-grade precision and consistency therefore bring in scientific instruments, moving from an assessment based on impression to one based on numbers that can be checked and compared. This lets the mill hold the colour of each roll as close as possible to the standard the customer specified.
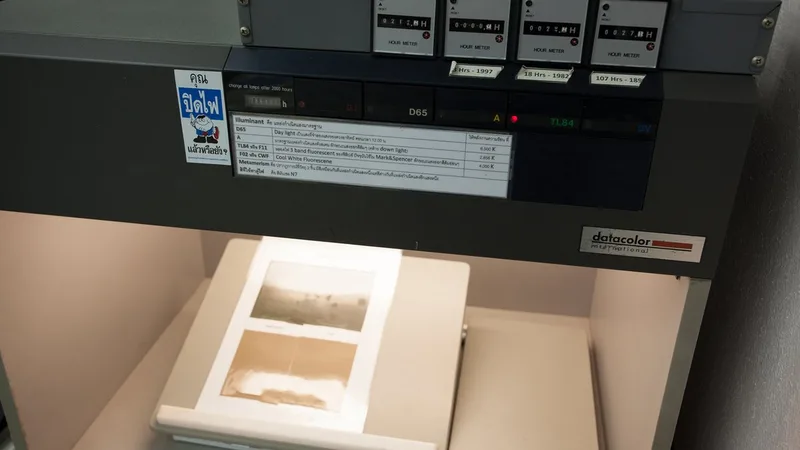

Why standard lighting matters when assessing fabric colour
The light used to judge colour is another decisive factor in lab dip approval. The same fabric colour can look different under different light sources. A mill may see a match to standard in the light box, but when the customer views the sample in an office, a shop or a showroom lit differently, the colour can appear more yellow, more blue, darker or lighter.
The phenomenon where two colours match under one light source but differ under another is called metamerism. Mill and customer should therefore agree the viewing conditions before the lab dip is approved, so that everyone is judging under the same terms.
Standard light sources commonly used for fabric
- D65
Standard daylight — commonly the primary light source for assessing textile colour. - TL84
Simulates shop and department-store lighting; widely used in European markets. - CWF
Cool white fluorescent; commonly used in the American market. - A / Warm Light
Incandescent or warm-toned light, simulating interior lighting. - UV
Used to check for fluorescent agents or optical brighteners on the fabric.
In general, D65 should be set as the primary light source for colour approval, with additional checks under TL84, CWF or A to match where the product will actually be seen. Checking under several lighting conditions reduces the risk of a colour that shifts in appearance, and of goods being rejected later.

The same fabric compared under each type of standard light
What is Delta E, and how does it relate to a lab dip?
For industrial colour assessment, a mill can use a spectrophotometer to measure the difference between the reference standard and the dyed sample. That difference is expressed as Delta E (ΔE).

Delta E turns colour assessment from a visual impression into a number that can be compared and tracked. The lower the Delta E, the closer the sample is to the standard. The appropriate acceptance threshold varies with fabric type, the nature of the product, and each brand’s own requirements.
Delta E levels and acceptance in textile work
- 0.0 – 1.0
Excellent. The difference from standard is so small it is barely distinguishable by eye. - 1.1 – 2.0
Good. Generally acceptable for most work, subject to the customer’s requirements. - Above 2.0
Needs further consideration, as the colour difference may be clearly visible.
Note: the Delta E ranges above are an initial guide. Acceptable tolerance should follow the standard and specific requirements of each brand or customer.
Key steps before approving a lab dip
For colour approval to work, mill and customer should agree the important details from the outset: the reference standard used for comparison, the fabric type and construction, the viewing conditions, the standard light sources, and the acceptable Delta E threshold.
Once the lab dip sample is ready, it should be checked both visually in a standard light box and against spectrophotometer data. Where a difference is found, the observation should be recorded and the dye recipe adjusted before the sample is submitted for approval. Retaining the approved sample as evidence also gives production and quality control a single shared standard for the life of the project.
In summary: the lab dip is the heart of fabric colour control
A lab dip is not simply a colour swatch to look at. It is a quality-control process that lets mill and customer agree a shade on the same basis before a large lot is produced. Done systematically, it reduces the risk of off-shade fabric, cuts the cost of re-dyeing, and gives confidence that what is delivered meets specification.
Alongside the lab dip itself, agreeing standard lighting for colour assessment and using Delta E from a spectrophotometer are what raise colour control to something precise, verifiable, and suited to international textile standards.
Boonchuay Industry Co., Ltd. is a full-cycle textile mill — weaving, scouring, dyeing, printing and finishing — with a laboratory for colour analysis and development, a spectrophotometer, and standard light boxes for colour assessment, so customers can be confident of fabric that matches specification, stays consistent, and competes in world markets.