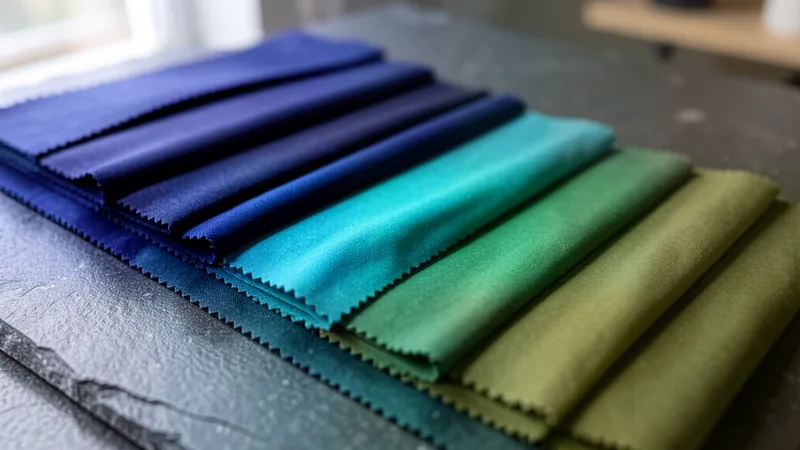
A fabric's colour does not come from the cloth alone — it is the interaction between the fibres, the dye and the light falling on it. A Pantone number is therefore only the starting point: bulk production also needs an agreed shade tolerance, and the shade must be checked under more than one light source before approval.
What is Pantone, and how is it used for fabric?
Pantone is the standard colour-identification system used across the fashion and textile industries. In the PANTONE Fashion, Home + Interiors (FHI) system, every shade has a unique number and name — for example 15-1247 Tangerine — so buyers, mills and suppliers across the world speak the same language without re-explaining a colour.
For fabric, the key reference is PANTONE TCX (Textile Cotton): real dyed cotton swatches. The same colours also exist as paper lacquer (TPG, formerly TPX), but dyed fabric and printed paper do not render a number identically — and Pantone's own guidance is to use TCX as the primary reference for fabric applications. TPG paper chips are for hard surfaces and office review. Every FHI colour is also supported by published spectral data, so the reference can be checked numerically, not just by eye.
The important point: a Pantone number is a starting point, not an approved standard. Dyeing is a chemical process — the shade that comes off the line depends on the fibre, the construction and the dye recipe. That is why production jobs are always approved on the mill's lab dip first. See our article on lab dips: controlling fabric colour before bulk production for the full process.
Shade tolerance: how close is close enough?
Shade tolerance is the maximum colour difference accepted between the produced fabric and the colour standard it is compared against. It is measured with a spectrophotometer, which reads the fabric's reflectance across the spectrum and calculates a colour difference — ΔE in the CIELAB colour space.
The standards used for this:
- AATCC EP7 — the instrumental assessment of colour change, using CIELAB values under D65 illuminant and the 10° observer; the instrumental alternative to visual grey-scale rating
- ISO 105-J03 — the textile method for calculating ΔE CMC(l:c), which lets a specification set a maximum tolerance based on the closeness of match the end use requires, independent of which colour is involved
There is no single "right" tolerance number; it depends on two things:
- The end use — fabric cut from several rolls and sewn into one product (a uniform, for example) needs tighter control than fabric used from a single roll
- The buyer's specification — many brands and buying houses state their tolerance in the product spec already
When ordering a dyeing job, state the tolerance in the spec, and agree with the mill how it will be measured (ΔE, CMC, or rating in a light booth). The customer-approved lab dip then becomes the working colour standard for the whole run.
Metamerism: the match that fails in daylight
Metamerism is when two samples look identical under one light source but different under another. It happens because the two samples have different spectral reflectance curves — their reflected wavelengths do not match, even though the visual impression does under a given light. It is most common when different dyes or raw materials are involved: matching thread to fabric, or matching two lots dyed with different recipes.
How to guard against it:
- Compare the pair side by side in a multi-illuminant standard light booth (for example D65 simulated daylight and TL84 retail lighting). If the match holds under every source, the risk is low
- Measure with a spectrophotometer and calculate a metamerism index (MI). As a rule of thumb cited by HunterLab, an MI below 0.5 indicates an acceptable match, between 0.5 and 1 needs closer examination, and above 1 the pair is not a suitable match
- Peer-reviewed work in MDPI found that two light booths with the same nominal colour temperature but different spectral power distributions can give different visual results — so a calibrated booth and an instrumental check together are the reliable combination
Why the same Pantone number can still look different
- Different substrates — the same number on TCX cotton and TPG paper is not an identical shade; each material takes colour differently
- Different fabrics — different fibres and constructions take the same dye to different depths and vibrancies, so a shade approved on one cloth needs its own check on another
- Different lighting — the same fabric reads warmer or cooler under office light, shop light or daylight
- Between lots — dyeing has process variables. A mill that controls well works from the approved lab dip and checks shade in-process on every lot
Our colour lab at Boonchuay Industrial
Boonchuay Industrial runs commission dyeing (เรารับย้อมผ้า) at its Sam Phran mill in Nakhon Pathom. A job can start three ways: (1) a colour specification, (2) a physical sample to match, or (3) a standard colour chosen from Boonchuay's swatch cards.
The colour lab provides:
- Colour analysis with a spectrophotometer and a multi-source light booth
- Dye recipe development with an automatic lab colour dispenser
- Trial dyeing in the laboratory in both continuous and batch mode, duplicating the mass-production process
Every production lot is checked against the customer-approved standard before release, under a three-stage quality control system: greige inspection, in-process checks and inspection at packaging, with a 10-point quality report.
FAQ
Can I just send a Pantone number? Yes, but also send a physical colour standard — TCX swatches are ideal — because the same number on paper and on fabric is not identical. The mill will dye a lab dip and match it against your reference under standard lighting before approval.
What shade tolerance should I set? It depends on the end use and your end customer's specification. ISO 105-J03 provides the method for setting a maximum tolerance per application — state it in the spec and agree the measurement method with the mill.
The sample matched in the office but looks off in the shop That is a metamerism signal. Compare the samples in a multi-illuminant booth (D65, TL84) and ask for the metamerism index from the spectrophotometer; if the MI is high, the dye recipe needs adjusting until the shade holds under every light source.
Can you dye my own fabric to a Pantone colour? What is the minimum order? Yes — we take commission dyeing work, and colour is always approved on a lab dip before bulk. The minimum order (MOQ) is negotiable: it depends on the fabric, the colour, the finish and the volume.
How is colour held consistent across large, multi-lot orders? The approved lab dip is the standard for the job, shade is checked in-process at every step, and our in-house lab measures colour values itself — all under ISO 9001 quality management.
References
- PANTONE Color Systems for Product Design (Fashion, Home + Interiors: TCX cotton, TPG paper, spectral data) — Pantone, pantone.com/products/fashion-home-interiors
- AATCC EP7:2021 — Instrumental Assessment of the Change in Color of a Test Specimen — AATCC, aatcc.org
- ISO 105-J03:2009 — Textiles: Tests for colour fastness — Part J03: Calculation of colour differences — ISO, iso.org
- A Comparison of Two Different Light Booths for Measuring Color Difference of Metameric Pairs — MDPI (peer-reviewed), mdpi.com
- Color Matching Challenges in Textiles: Detecting Illuminant Metamerism — HunterLab, hunterlab.com
If you are looking for a dyeing partner for uniform fabrics, workwear or fabric to your own specification, see our full commission dyeing and finishing services and contact the Boonchuay team to send your specification and colour reference.